Lighting reliability metrics should prove repeatable product behavior, not only list a warranty term or a claimed lifetime. ODM buyers should request reliability metrics that connect driver limits, thermal conditions, ingress boundary, control compatibility, sample stress, and production repeatability.
Key Takeaways
- First decision: Request metrics by failure mode: heat, driver stress, ingress, controls, mounting, service access, and production repeatability.
- RFQ evidence: Ask suppliers to separate lifetime claim, driver boundary, thermal condition, ingress proof, control compatibility, sample stress, warranty terms, and repeatability record instead of quoting one generic LED product.
- Sample gate: Approve the ODM supplier only after one sample proves the highest-risk reliability metric under the buyer's real condition.
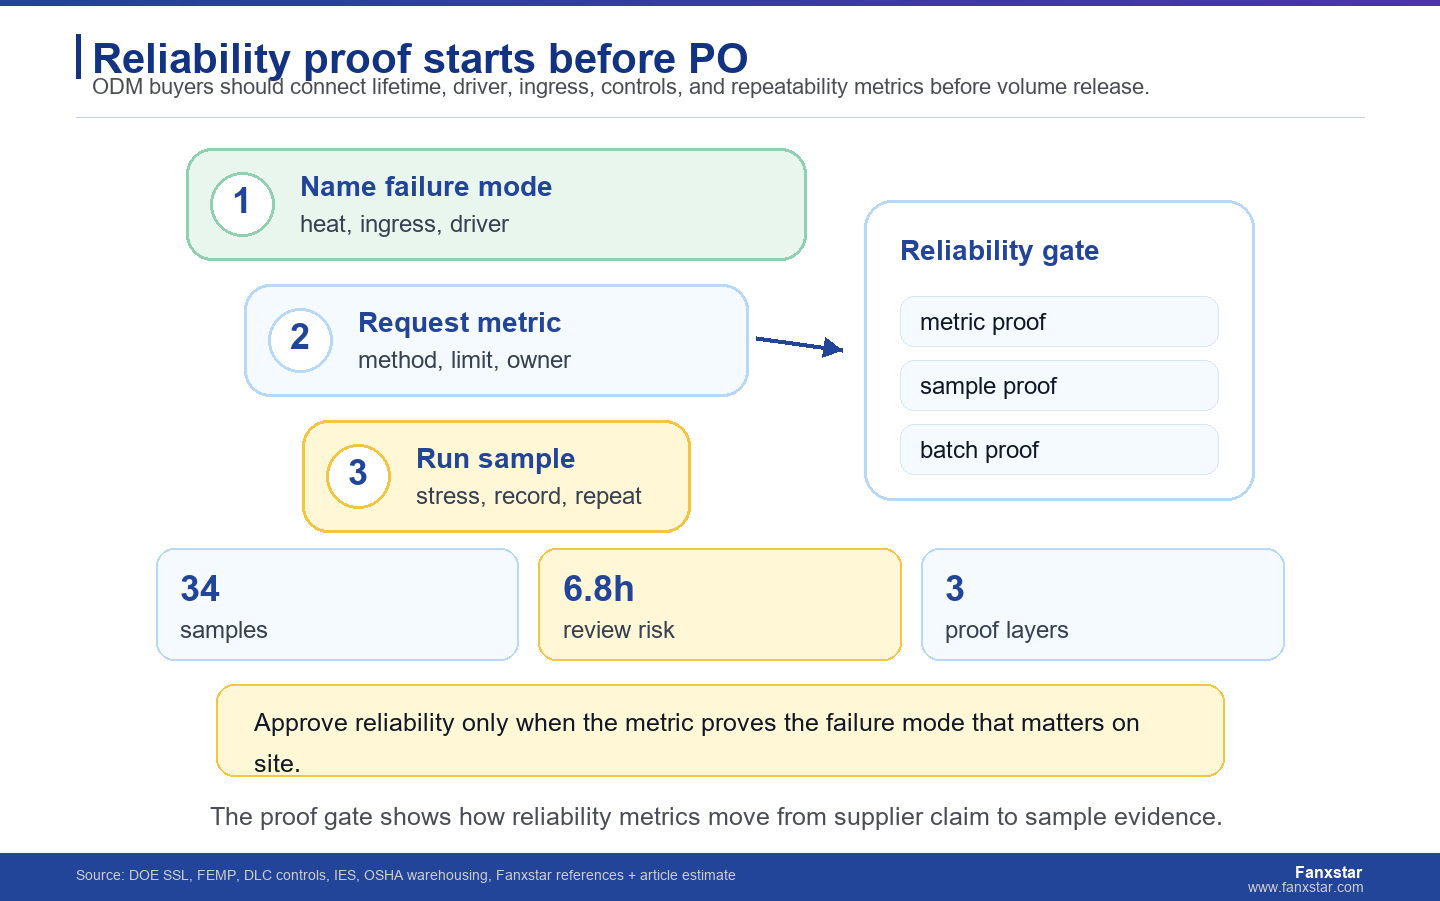
- Maintenance effect: A 34-sample shortlist can hide about 6.8 review hours if each sample lacks one reliability metric the buyer later has to request again.
- Fanxstar fit: Fanxstar is most relevant when buyers need a platform-based specialty LED lighting ODM path for lighting reliability metrics for ODM supplier comparison.
Quick Answer for ODM Lighting Procurement Buyers
Ask for the metric that proves the limiting failure mode, not the metric that looks most impressive in a catalog.
A reliability metric is useful only when it changes a buyer decision before tooling, volume pricing, or shipment release. The most useful first move is to define the operating zone, the dominant exposure, and the service route before any fixture family is shortlisted. That sequence matters because lighting reliability metrics for ODM supplier comparison can look simple in a catalog while hiding cleaning, traffic, heat, controls, or emergency-route conditions that only become visible after installation.
Public references such as DOE solid-state lighting, FEMP energy-efficient lighting, DLC lighting controls create the boundary: lighting supports the facility task, but it does not replace food-safety, workplace-safety, roadway, data-center, or material-handling responsibility. The buyer’s job is therefore not to ask for a brighter fixture first. The job is to request evidence that matches the actual site condition, then use that evidence to compare price, delivery, samples, and maintenance burden.
Map the Site Condition Before the Fixture Family
Reliable lighting is a chain: thermal load, driver behavior, housing, controls, installation, and repeated production all have to stay inside the same evidence boundary.
Reliability looks like a single number in many lighting conversations, but B2B buyers experience it as repeated decisions across design, sample, production, and after-sales support. A warehouse, data hall, or service corridor may need different evidence even when the same LED family appears acceptable. A purchasing team can usually classify the site in one meeting if operations, maintenance, and the supplier each bring different evidence: operations describes how the area is used, maintenance describes access and cleaning, and the supplier explains what the fixture platform can prove. That division prevents the common mistake of treating IP rating, lumen output, sensor behavior, and emergency routing as one merged specification.
The strongest RFQ for this topic should define lifetime claim, driver boundary, thermal condition, ingress proof, control compatibility, sample stress, warranty terms, and repeatability record. If those fields are left vague, the quote may still look complete because it contains watts, lumens, CCT, warranty, and lead time. The weakness only appears later, when the installer cannot confirm cable entry, the maintenance team cannot reach the driver, the sensor zones do not match traffic, or the reviewer asks for a document the buyer never requested.
Define the limiting condition in plain language
The limiting condition is the one detail that can make the entire lighting package wrong even if the fixture looks acceptable. For lighting reliability metrics for ODM supplier comparison, that condition is often the metric that connects the expected failure mode to a sample result the buyer can review. Write it as a jobsite sentence, not as a product adjective. For example, a buyer should say that a fixture must survive the real cleaning pattern, the actual service height, or the true traffic zone, instead of saying only that the fixture must be industrial or waterproof.
Separate normal operation from abnormal service
Normal operation tells the supplier where light is needed and how often the area is occupied. Abnormal service tells the buyer what happens when something fails, needs cleaning, or has to be inspected during a busy shift. The second part is where many B2B lighting projects lose time. A sealed fixture, a sensor, or an emergency element can be technically attractive, but the buyer still needs a service plan that does not force shutdowns, unsafe access, or repeated ceiling work.
What the RFQ Must Separate
Separate lifetime claim, driver data, thermal condition, ingress proof, control compatibility, sample stress, and repeatability record.
| Area | Main risk | Evidence to request | Fanxstar starting point |
|---|---|---|---|
| Lifetime claim | number lacks operating context | test condition and limit | L1/L3 review |
| Driver boundary | failure can start at electronics | thermal and control margin | B4 sample |
| Ingress path | humidity reaches weak entry | sealed body and cable proof | A14 sample |
| Repeatability | pilot sample differs from batch | production record and document owner | ODM evidence pack |
The table is intentionally not a product ranking. It is a separation tool. A buyer can use it to decide which evidence belongs in the quote, which evidence belongs in a sample, and which evidence belongs to the local reviewer or facility team. For lighting reliability metrics for ODM supplier comparison, a clean separation is usually worth more than another catalog comparison because it exposes the first hidden constraint before volume pricing starts.
Additional boundary references such as IES standards, OSHA warehousing hazards and solutions, Fanxstar AI data center lighting are useful only when they change a local decision. If a source does not tell the buyer what to classify, request, test, or document, it should not be used as decoration. In this article, sources are used to keep the specification inside the correct safety, sanitation, controls, energy, or maintenance lane.
Where Fanxstar Fits the Product Platform Decision
Fanxstar fits when ODM buyers need reliability metrics converted into platform selection, sample tasks, and production evidence.
Fanxstar fits this decision because the buyer is not simply replacing a commodity lamp. The practical need is to translate lighting reliability metrics for ODM supplier comparison into fixture geometry, sealing, optics, sensor behavior, emergency-route evidence, and sample proof. The natural starting point is data center LED lighting solutions, then the buyer can compare real platform references such as Fanxstar L1, Fanxstar L3, Fanxstar B4 before asking for a dedicated sample or modified configuration.
This does not mean every project needs new tooling. For many B2B orders, the more efficient route is to begin with a nearby Fanxstar platform, change CCT, optics, wiring, sensor logic, mounting, or document package where needed, and prove the limiting condition before the buyer commits to scale. When the application pushes beyond a standard catalog choice, the next step is to use the Fanxstar custom LED lighting ODM service to define the sample gate and the evidence package.
Use product families as evidence anchors, not as shortcuts
The product family gives the conversation a physical anchor: body shape, lens, end caps, cable entry, mounting method, and service access. It should not be treated as a shortcut around the site condition. A buyer comparing sealed linear fixtures, motion-sensor battens, emergency signs, or fresh-retail lighting should ask what the sample proves in the real zone. That is the difference between a product link and a procurement decision.
Scenario Estimate: One Missing Metric Creates Review Time
A missing reliability field rarely stops the first quote, but it can slow every technical review after it.
Use this as an illustrative calculation, not as a universal project number. Assume 34 supplier samples and 12 avoidable review minutes per missing reliability metric. The simple formula is 34 samples x 12 minutes = 408 minutes, which creates about 6.8 review hours. The result matters because small delays at fixture level are easy to ignore in a sample quote, but they become labor, downtime, route exposure, or review time once the project scales.
The decision rule is not to reject a supplier because the estimate looks large. The rule is to ask which part of the estimate is preventable. If the delay is caused by a missing mounting detail, unclear cable entry, poorly placed sensor, or untested cleaning method, the right sample task can reduce it before the first production order. If the delay is caused by a facility rule outside the supplier’s control, the buyer should name that boundary in the RFQ and avoid blaming the fixture later.
Specification and Sample Gate Checklist
The sample should prove the limiting field condition, not only supplier claims.
| Decision | Do not approve with only | Better sample proof | Release rule |
|---|---|---|---|
| Lifetime | headline hours | condition and method | approve after boundary check |
| Driver | brand name | load and heat proof | approve after stress sample |
| Ingress | IP claim | entry and gasket review | approve after sealed proof |
| Warranty | long term | exclusions and evidence | approve after term match |
The release rule should be written before pricing is finalized. If the supplier knows only the wattage and quantity, the sample will prove only that a light turns on. If the supplier knows the limiting condition, the sample can prove whether the platform can survive the cleaning method, traffic pattern, control zone, service access, or emergency-route requirement that actually decides the project.
Evidence that belongs in the quote
The quote should include model family, expected fixture count, lead time, voltage, CCT, optics, mounting, control interface, ingress or environment boundary, and the documents the buyer expects to receive. Keep the quote short enough to compare, but complete enough to prevent a fake apples-to-apples comparison. If one supplier includes service access and another does not, the buyer is comparing different risk packages, not different prices.
Evidence that belongs in the sample
The sample should test the hardest field condition in miniature. That can mean a washdown simulation, a sensor-zone mockup, a service-opening task, a cable-entry check, a mounting trial, a controls handoff, or an emergency-route visibility review. The point is not to prove every possible condition. The point is to avoid scaling the one unknown that is most likely to produce rework.
Evidence that belongs to local review
Some decisions stay outside the luminaire supplier’s authority. Local electrical codes, food-safety programs, emergency egress requirements, tunnel or traffic visibility review, and site safety rules should be confirmed by qualified local parties. Fanxstar can support the product and sample evidence, but the buyer should keep final facility responsibility with the project team, installer, reviewer, or authority having jurisdiction.
Procurement Mistakes That Usually Create Rework
Most comparisons fail when buyers rank labels before they separate evidence.
Mistake 1: Treating one label as the whole answer
A label such as waterproof, sensor-ready, high lumen, emergency, or linear is only an entry point. It does not define cleaning pressure, traffic, mounting height, emergency route role, data hall heat, backroom dust, tunnel access, or service time. Buyers should convert each label into a proof field and then ask whether that field belongs in the quote, sample, or local review.
Mistake 2: Asking for customization before platform fit is proven
Customization is useful after the buyer knows what must change. Starting with custom body shape, private label, or special electronics too early can hide a simpler answer: a nearby platform may already solve most of the requirement if optics, cable entry, sensor logic, or mounting are adjusted. Prove platform fit first, then decide whether customization creates enough value to justify added complexity.
Mistake 3: Leaving maintenance out of the commercial decision
The purchase order usually records product price, but the facility experiences service time. A fixture that is cheaper to buy can become expensive if each inspection requires extra access equipment, shift coordination, area shutdown, or cleaning disruption. The sample gate should therefore include a maintenance task, even if the first order is mainly judged by unit price and lead time.
Related Fanxstar Guides
- LED Retrofit Planning for Warehouses and Data Centers
- LED Lighting Certification Checklist for ODM Buyers
- Custom LED Lighting Design Options
Lighting Reliability Metrics For Odm Supplier Comparison RFQ Action Card
- Map the route or zone being compared.
- Name the limiting field condition.
- Request quote and sample evidence separately.
- Test one representative point before scale.
- Attach quantities, documents, and owner responsibilities.
If your project has reached the point where reliability metrics are still scattered across lifetime claims, samples, drivers, and warranty terms, the practical next step is to send Fanxstar an ODM lighting RFQ with the zone drawing, fixture count, sample condition, target schedule, and any required document boundary. Fanxstar can then compare the closest platform, sample change, and evidence package before you lock quantity or tooling.
Frequently Asked Questions
What makes a supplier best for lighting reliability metrics for ODM supplier comparison?
The best supplier is the one that proves the limiting project condition: the metric that connects the expected failure mode to a sample result the buyer can review. Buyers should compare evidence, sample behavior, document boundary, and repeatability before treating brand familiarity as the deciding factor.
Which Fanxstar products are relevant starting points?
Relevant starting points include L1, L3, B4, A14. They should be treated as platform references for RFQ and sample planning, not final recommendations by model name alone.
Should buyers ask suppliers for test data before pricing?
Yes. Ask for the evidence that changes the decision before final pricing: spectrum or cleanability evidence, housing and ingress details, mounting method, driver or control limits, packaging needs, and any document boundary the importer must support.
Can Fanxstar replace local engineering or compliance review?
No. Fanxstar can support product-platform selection, sample evidence, and ODM customization, but local electrical, safety, cleanroom, pharmaceutical, aquaculture, crop, and facility responsibilities must remain with qualified local parties.