You know safety stands as a top priority in semiconductor manufacturing. Amber lighting plays a vital role in protecting sensitive processes and reducing contamination risks. The Fanxstar IP65 Clean-room Amber Light uses advanced amber LED technology to deliver these benefits.
-
Amber light works at a 570nm wavelength, which shields photochemically sensitive materials from harmful UV and blue light.
-
Manufacturers use amber light to prevent premature hardening of coatings, which improves product quality and yield.
-
Amber lighting supports a clean environment by reducing unwanted exposure and interference.
When you install the Amber Teardrop Light G2, you strengthen your factory’s defenses against contamination and help maintain high standards.
Key Takeaways
-
Amber lighting protects sensitive materials by filtering out harmful blue and UV light, ensuring high product quality.
-
The Fanxstar teardrop luminaires is designed for cleanrooms, resisting dust and water while supporting frequent cleaning.
-
Using amber light reduces glare and eye strain for workers, creating a safer and more comfortable work environment.
-
This lighting technology enhances visibility during critical tasks like wafer inspection, improving accuracy and reducing defects.
-
Installing the IP65 cleanroom luminaire helps maintain compliance with industry standards, ensuring a safe and efficient manufacturing process.
Amber Lighting in Semiconductor Manufacturing
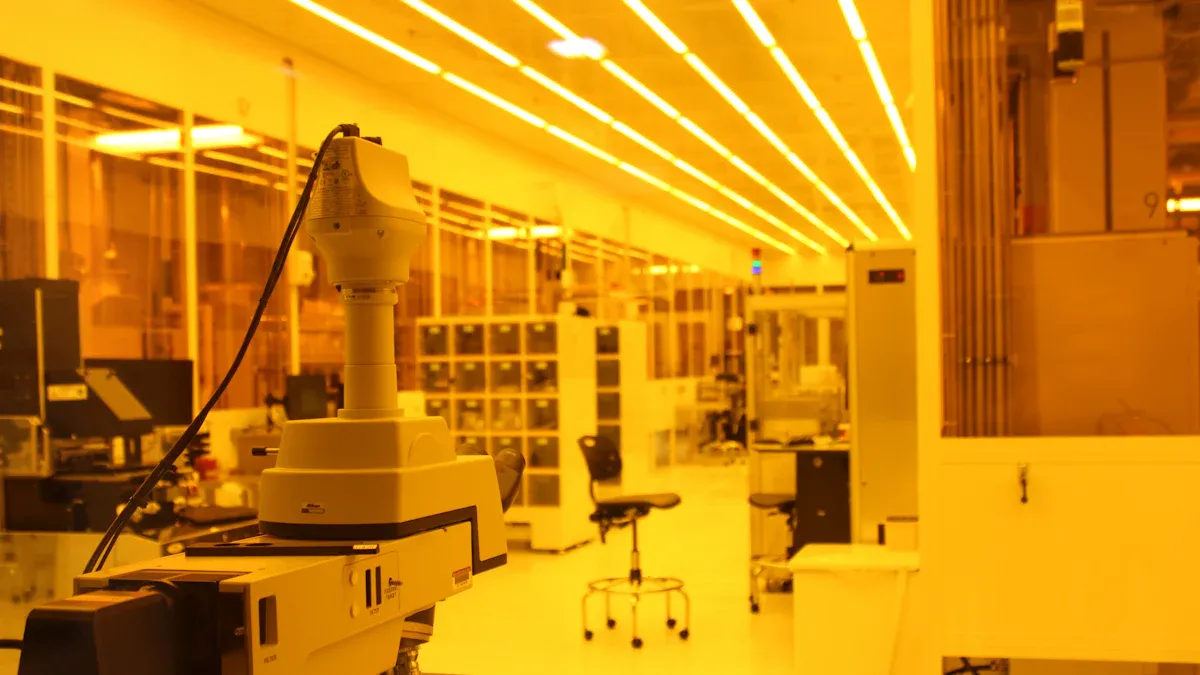
Photosensitive Process Protection
You work in semiconductor manufacturing, so you know that protecting sensitive materials is critical. Many processes use photo-resists, which react to certain wavelengths of light. If you expose these materials to blue or ultraviolet light, you risk damaging them or causing unwanted reactions. Amber lighting provides a solution by filtering out these harmful wavelengths.
Amber lighting operates in a specific wavelength range that keeps your photosensitive materials safe. The optimal range for this purpose falls between 590nm and 570nm. This range blocks out blue and UV light, which can interfere with photo-lithography and other sensitive steps.
Here is a quick overview:
|
Wavelength Range |
Purpose |
|---|---|
|
Filters out damaging blue and UV light to protect photo-resists in semiconductor manufacturing |
You use amber lighting in areas where you handle photosensitive materials. This approach prevents accidental exposure and helps you maintain high product quality. When you rely on amber light led systems, you create an environment that supports precise and reliable semiconductor manufacturing.
-
Amber lighting is specifically utilized in environments where photosensitive materials are present to prevent exposure to harmful wavelengths.
Amber Light LED Benefits
Amber light led technology brings several advantages to your semiconductor manufacturing facility. First, these lights prevent unwanted exposure during photo-lithography. You avoid costly errors and reduce the risk of defects in your products. Amber light led fixtures emit light only in the safe wavelength range, so you do not have to worry about accidental contamination from stray blue or UV light.
You also benefit from improved visibility. Amber lighting reduces glare, which helps your workers see clearly and perform tasks with greater accuracy. This lighting creates a comfortable environment, which supports productivity and safety. When you use amber light led systems, you eliminate blue light, which can cause eye strain and interfere with sensitive processes.
You can count on amber lighting to deliver consistent performance. The technology supports the strict requirements of semiconductor manufacturing. You maintain control over your environment, protect your materials, and ensure that every step meets industry standards.
Amber Light Fixture Features
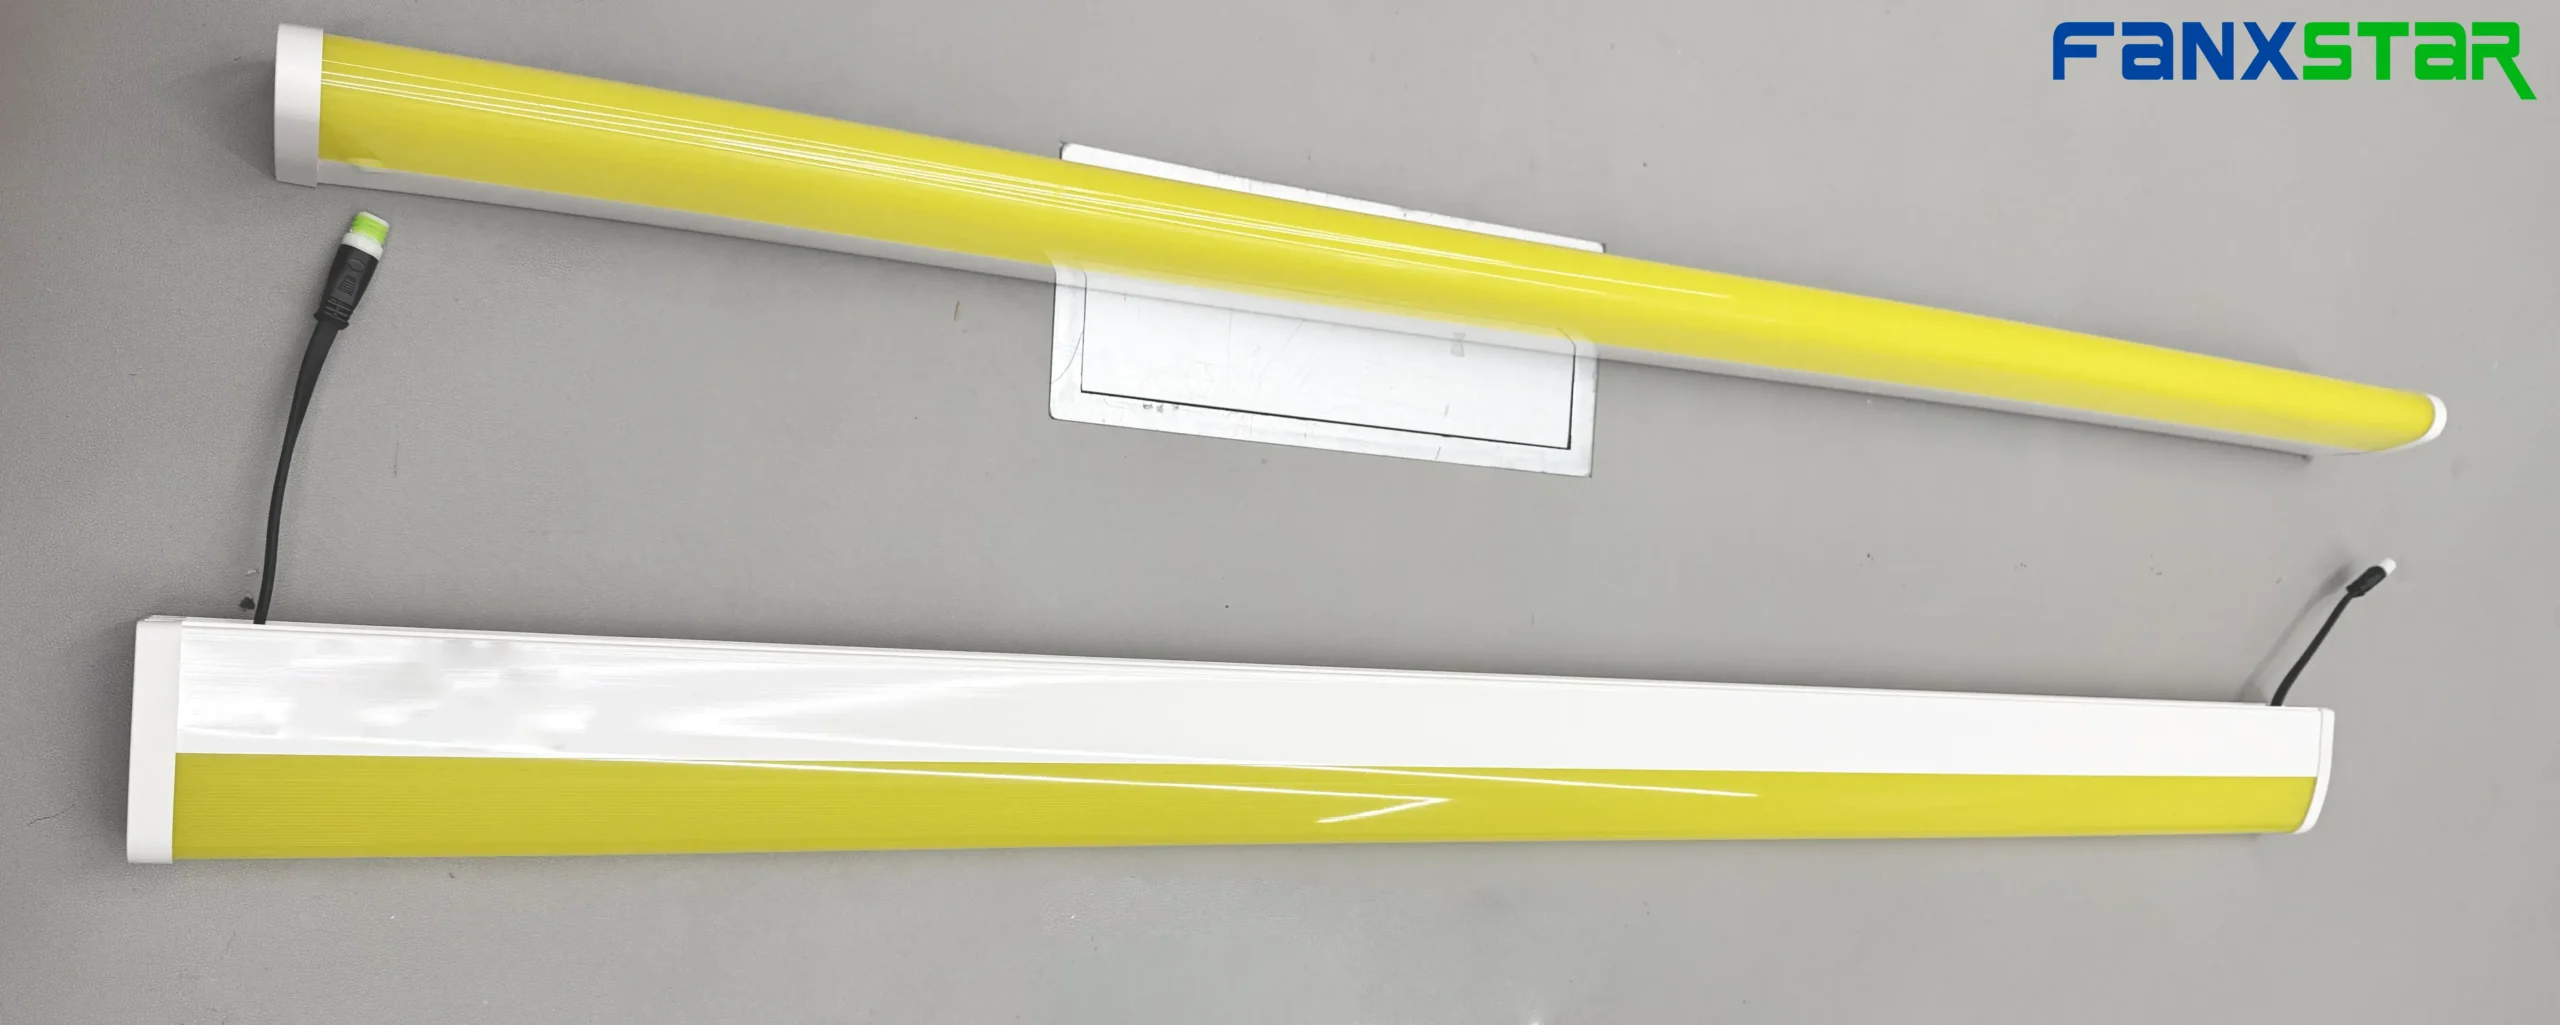
Durability
You need lighting that stands up to the demands of semiconductor manufacturing. The cleanroom light with Amber lens gives you this durability. Its design meets the strict requirements of cleanroom environments. The ip65 amber light uses a sealed structure and anti-bacterial coating. This helps the fixture resist dust, water, and caustic cleaning agents. You can clean the led fixture with water without worrying about damage. The cleanroom luminaire keeps working even after frequent cleaning cycles.
-
The amber light is built for cleanrooms.
-
The led housing resists dust and water.
-
The sealed design prevents contamination.
-
The anti-bacterial coating supports hygiene.
-
The amber lens of the led protects photo-resist materials.
-
Emergency backup battery and Motion Sensor as optional.
You can rely on the ip65 amber light for long-term performance. The led system maintains high output and stable color. This means you get consistent illumination for your sensitive processes. The led technology also reduces maintenance needs. You spend less time replacing fixtures and more time focusing on production.
Environmental Protection
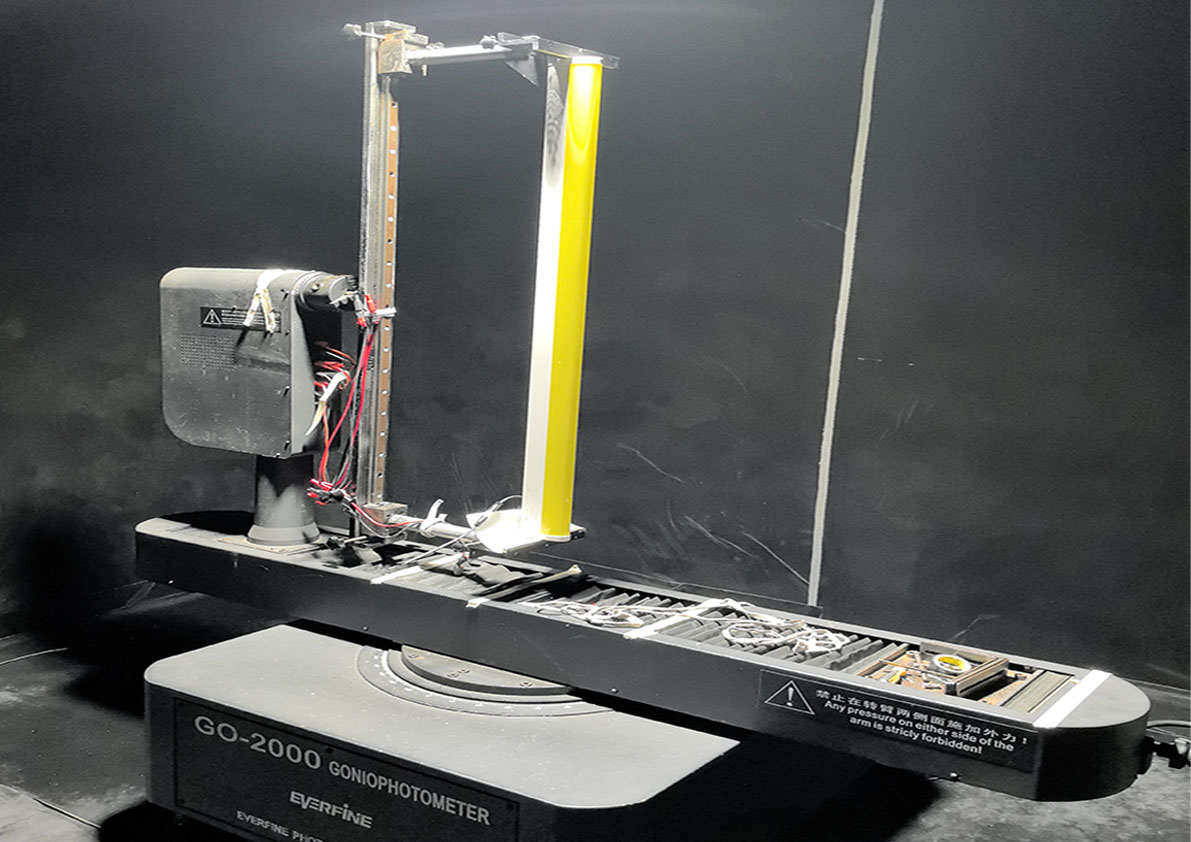
Lighting in semiconductor cleanrooms must meet strict environmental standards. The amber light delivers on all fronts. You get a fixture that protects both your process and your environment. The led system uses a teardrop-shaped design. This shape keeps airflow smooth and supports laminar flow in your cleanroom.
Here is how the amber luminaire meets cleanroom requirements:
|
Feature |
Description |
|---|---|
|
Ensures dust and water resistance, crucial for cleanroom environments. |
|
|
Amber Lens Lamps |
Filters <500nm wavelengths to protect light-sensitive materials in semiconductor applications. |
|
Airflow-Optimized Structure |
Teardrop-shaped fixture design maintains laminar flow integrity, essential for cleanroom standards. |
|
Compliance with ISO Standards |
Meets strict ISO 14644 standards for air cleanliness and other industry-specific regulations. |
|
Sealed Design |
Contamination-resistant design that supports precise semiconductor manufacturing processes. |
|
0-10V Dimming |
Adjust brightness smoothly to suit any environment or task, all with advanced digital reliability. |
The led system provides uniform light for high-ceiling areas. You can use the teardrop cleanroom lumianire in electronics manufacturing rooms and even cold storage. The led fixture keeps your workspace bright and safe. You protect your products and your workers with every installation.
Safety Advantages of Amber Light
Contamination Prevention
You face many challenges in semiconductor manufacturing. One of the biggest risks comes from contamination. Even a small amount of unwanted light can damage photochemically sensitive materials. Amber lighting gives you a powerful tool to fight this risk. When you use amber lighting, you block out harmful blue and ultraviolet wavelengths. This action protects your materials from photo-oxidative damage and keeps your processes stable.
Researchers have studied how amber lighting affects sensitive environments. The results show that amber lighting reduces oxidative stress and changes protein expression. This effect helps prevent damage to your materials. The table below summarizes some important findings:
|
Evidence Description |
Findings |
|---|---|
|
Biostatic effect of amber and green light |
The combination reduces oxidative stress and alters protein expression, mitigating damage to sensitive materials. |
|
Induction of oxidative stress |
Exposure to amber + green lighting at night leads to a stress response in organisms, indicating protective effects against contamination. |
|
Photo-oxidative damage |
Stress emerges from an imbalance in light energy received versus utilized, highlighting the protective role of amber lighting during darkness. |
You can see that amber lighting does more than just illuminate your workspace. It acts as a shield for your photochemically sensitive materials. By using amber lighting, you lower the risk of contamination and improve your product yield. You also create a cleaner environment for your entire facility.
Worker Safety
You want your team to work safely and efficiently. Amber lighting helps you achieve this goal. Many workers experience eye strain and fatigue when exposed to harsh blue or white lighting. Amber lighting creates a softer, more comfortable environment. This type of lighting reduces glare and improves visibility, especially in areas where precision matters.
When you install amber lighting, you help your workers see details clearly. Tasks like inspecting wafers or assembling components become easier. You also lower the chance of mistakes caused by poor visibility. Amber lighting supports your team’s well-being by minimizing eye discomfort and supporting focus.
You can rely on amber lighting to maintain a safe workspace. The consistent color and brightness of amber lighting make it easier for workers to spot hazards. You also reduce the risk of accidents caused by glare or shadows. Amber lighting gives you a simple way to protect both your products and your people.
Tip: Choose amber lighting for your cleanroom to support both contamination control and worker safety. You will notice improvements in both product quality and employee comfort.
Installation and Maintenance
Cleanroom Compatibility
You want lighting that fits seamlessly into your cleanroom. The Fanxstar Amber Light makes installation simple. You can mount these fixtures on ceilings or walls without special tools. The compact design lets you place them in tight spaces. You do not need to worry about airflow disruption. The teardrop shape supports laminar flow, which is essential for keeping your cleanroom free from particles.
You can clean the ip65 rating Amber Lamp with standard procedures. The sealed housing resists dust and water, so you can use wet cleaning methods. The anti-bacterial coating helps you maintain hygiene. You save time because you do not need to remove the fixture for routine cleaning. This design keeps your clean-room running smoothly and reduces downtime.
Tip: Choose lighting that supports your cleanroom’s airflow and cleaning protocols. You will see fewer interruptions and better process control.
Reliability
You need lighting that performs reliably every day. The Fanxstar IP65 Amber Luminaire meets strict industry standards for durability and efficiency. You can check its reliability using several key metrics:
|
Metric |
Description |
|---|---|
|
IP Ratings |
Protects against dust and water (IP65 is ideal for cleanrooms). |
|
CRI Values |
High color accuracy (above 90) for precise work. |
|
Lumens-per-Watt Efficacy |
High efficiency (up to 160 lm/W) saves energy. |
|
Thermal Management |
Prevents overheating and extends lifespan |
|
L70 Lifespan Ratings |
Long life—keeps 70% brightness for tens of thousands of hours. |
|
Quality Assurance |
Factory audits and ISO 9001 certification ensure consistent performance. |
|
Photometric Distribution |
Even light spread for safe, clear visibility. |
|
Driver Performance |
120-277Vac Universal Voltage with low flicker (below 5% at 100Hz) for worker comfort and safety. |
You can trust the Fanxstar IP65 Cleanroom Lighting to deliver stable, bright illumination for years. You spend less time on maintenance and replacements. This reliability helps you keep your production line efficient and your cleanroom safe.
Case Studies and Feedback
Real-World Applications
You see the Fanxstar IP65 Amber Light in action across many semiconductor manufacturing facilities. These factories rely on amber light led solutions to protect sensitive processes. In one leading semiconductor plant, you use amber lighting in wafer inspection rooms. This approach ensures that photochemically sensitive materials stay safe during every process step. You also find amber illumination in alignment stations, where precise lithographic alignment is critical. The consistent illumination from amber light led fixtures helps you reduce the risk of defect formation.
You use amber lighting in cleanrooms for both inspection and alignment. This lighting supports defect detection and helps you maintain high product quality. In another facility, you install energy-efficient lighting to improve wafer inspection accuracy. The amber light led system provides stable illumination, which is essential for process control. You notice that the amber illumination makes it easier to spot issues during inspection and alignment tasks.
Note: Amber lighting plays a key role in semiconductor manufacturing by supporting wafer inspection, alignment, and process stability.
Testimonials
Facility managers and engineers share positive feedback about the Fanxstar IP65 Amber Light. One manager says, “You improve inspection accuracy and reduce contamination risks with this amber light led system.” An engineer adds, “You rely on consistent illumination for every process, especially during wafer inspection and alignment.” Workers also report less eye strain and better visibility during long shifts.
You hear from another facility manager who values the reliability of the amber lighting. “You spend less time on maintenance and more time focusing on semiconductor manufacturing,” they explain. These testimonials highlight how amber illumination supports both safety and productivity in your semiconductor processes.
“You can trust amber light led fixtures to deliver stable illumination for every inspection and alignment task.” – Process Engineer
You see how the Fanxstar IP65 Cleanroom Light with amber lens transforms manufacturing environments. In semiconductor manufacturing, you need lighting that supports safety, compliance, and process integrity. The table below highlights key safety benefits:
|
Safety Benefit |
Description |
|---|---|
|
Industry-Leading Sterility & Compliance |
IP65+ rated seals prevent particle ingress, ideal for manufacturing and cleanroom environments. |
|
Dust- and Bacteria-Resistant Design |
Resists dust and bacteria, supporting frequent cleaning in manufacturing facilities. |
|
Safety and Compliance |
Yellow-tinted lamps protect light-sensitive materials in manufacturing processes. |
You follow expert recommendations for manufacturing by choosing amber lighting.
-
You protect photochemically sensitive materials in manufacturing cleanrooms.
-
You minimize unwanted wavelengths, ensuring manufacturing process integrity.
-
You filter out blue and UV light, preventing premature reactions in manufacturing photoresists.
-
You reduce light pollution, eye strain, and glare for manufacturing staff.
Amber lighting is now a vital trend in manufacturing, especially in semiconductor manufacturing. You ensure safety and consistency in manufacturing by adopting the Fanxstar IP65 Yellow Light. Consider this solution to keep your manufacturing facility safe, efficient, and ready for the future.
FAQ
What makes Fanxstar IP65 Amber Light suitable for cleanrooms?
You get a sealed design that resists dust and water. The fixture supports frequent cleaning and meets strict cleanroom standards. You maintain a sterile environment with reliable performance.
How does high-performance amber lighting protect semiconductor processes?
You shield sensitive materials from harmful blue and UV wavelengths. High-performance amber lighting ensures stable conditions for photolithography and wafer inspection. You improve product quality and reduce contamination risks.
Can you install solid-state amber illumination in existing facilities?
You can retrofit solid-state amber illumination into most cleanrooms. The compact design fits standard fixtures. You upgrade your lighting without major changes to your workspace.
Does amber lighting help reduce worker eye strain?
You experience less glare and softer light. Amber lighting creates a comfortable environment for long shifts. You support worker safety and improve visibility during detailed tasks.
How often do you need to maintain Fanxstar IP65 Amber Light fixtures?
You perform routine cleaning with standard procedures. The sealed housing and anti-bacterial coating minimize maintenance needs. You spend less time on replacements and repairs.